

Sulfuric Acid Systems
Your Experts in H2SO4 Dilution, Dewatering, and Regeneration
CG Thermal designs sulfuric acid process systems for dilution, concentration, and regeneration. Because sulfuric acid’s properties and corrosivity vary significantly with concentration and temperature, each system requires careful consideration of mixing, heat removal, process control, and materials of construction. Sulfuric acid is essential to fertilizer production, petroleum refining, metals processing, and industrial chemical manufacturing. Common applications include phosphoric acid production, refinery alkylation, ore leaching, steel treatment, dehydration, and pH control.
Industries & Applications
- Phosphoric acid and phosphate fertilizer production
- Petroleum refining and petrochemical processing
- Copper and zinc processing, including ore leaching
- Steel pickling, descaling, and surface preparation
- Production of esters and other industrial chemicals
- Nitration of toluene and other aromatic compounds
- Dehydration and moisture-removal processes
- Water and wastewater treatment and pH control
- Lead-acid battery manufacturing and recycling
- Pulp, paper, pigment, and detergent manufacturing
Sulfuric acid supports essential processes across fertilizer production, petroleum refining, metals processing, electronics, paper, and specialty chemical manufacturing. CG Thermal applies its heat- and mass-transfer expertise to systems that carefully manage acid concentration, temperature, mixing, and material compatibility. Our systems group can provide integrated process equipment or engineering support tailored to each application.

Sulfuric Acid Dilution
Diluting concentrated sulfuric acid with water generates substantial heat. A properly designed system coordinates mixing, heat removal, materials of construction, and process controls to achieve the required acid concentration, outlet temperature, and production rate.
CG Thermal provides custom-designed skid-mounted systems and pre-engineered DiluteMax Pro™ packages to meet a range of dilution requirements. We also offer process engineering support and individual components to complement your in-house capabilities. Explore the two system options below.
Custom Sulfuric Acid Dilution Systems
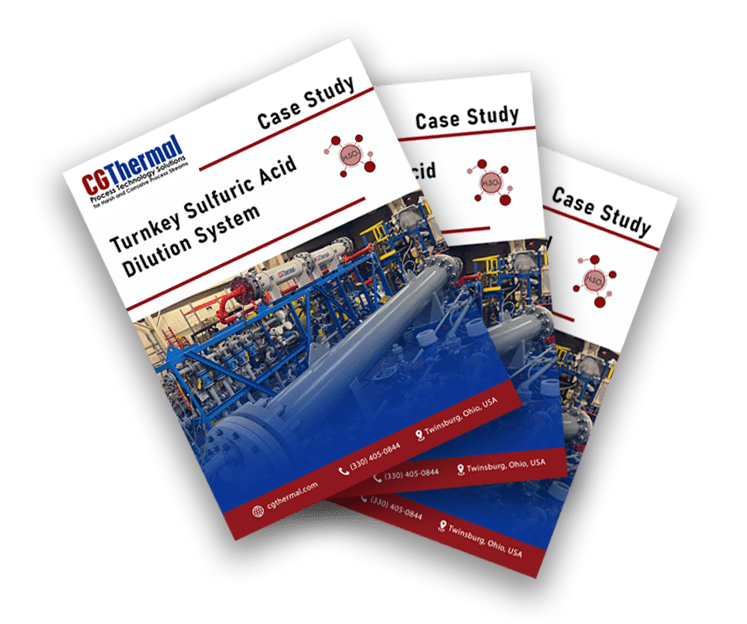
CG Thermal designs custom turnkey sulfuric acid dilution systems around your process requirements, plant layout, and existing infrastructure. Each skid-mounted system brings together mixing, cooling, instrumentation, and controls in an integrated package configured for your application.
System design options include:
- Capacity, outlet concentration, and temperature tailored to your process
- Mixing, recirculation, and heat removal arrangements selected for your operating conditions
- Instrumentation to monitor acid and cooling-water flow, temperature, concentration, and tank levels
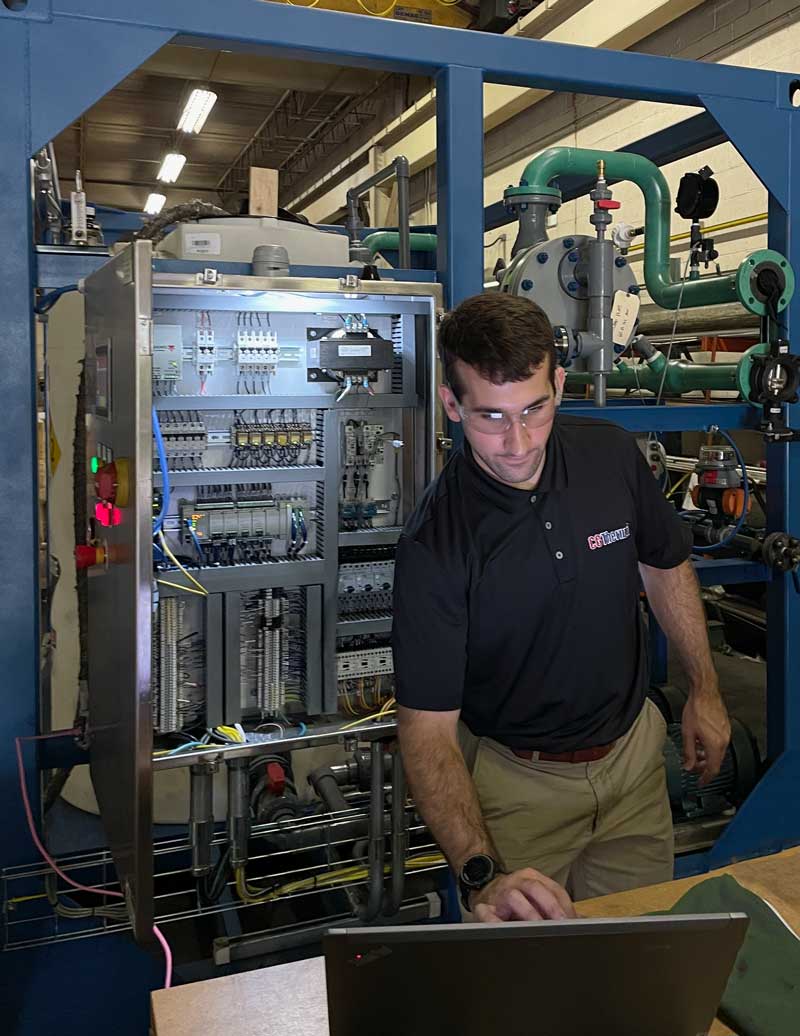
- Automated valve and pump controls, with local or remote operator interfaces and PLC integration compatible with your plant’s distributed control system (DCS)
- Storage tanks, transfer pumps, and connections to existing equipment as needed
Pre-Engineered Sulfuric Acid Dilution Systems
A Faster Path to Onsite Dilution.
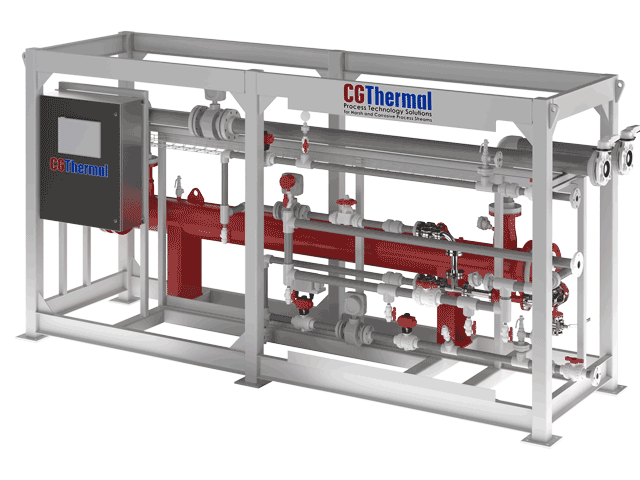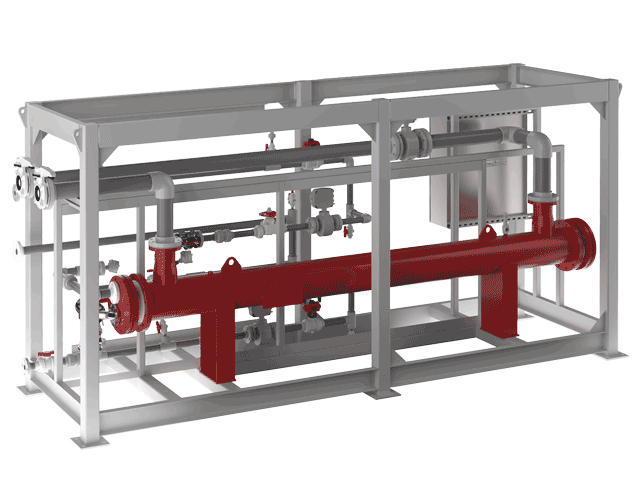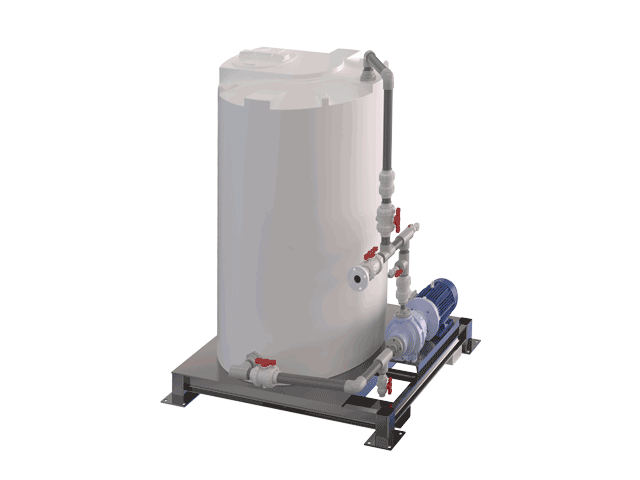
Produce the sulfuric acid concentration your process requires—right at your facility. CG Thermal’s DiluteMax Pro™ pre-engineered packages combine controlled acid and water metering, mixing, heat removal, instrumentation, and automated controls in an integrated skid-mounted system. Start with a defined package, then add tanks, pumps, or other equipment as your application requires.
- Integrated dilution process and Umax SiC Advanced Ceramic heat exchanger
- Pre-programmed PLC, instrumentation, and controls
- Optional storage tanks and pump skids
Umax: The Heart of Our Sulfuric Acid Systems
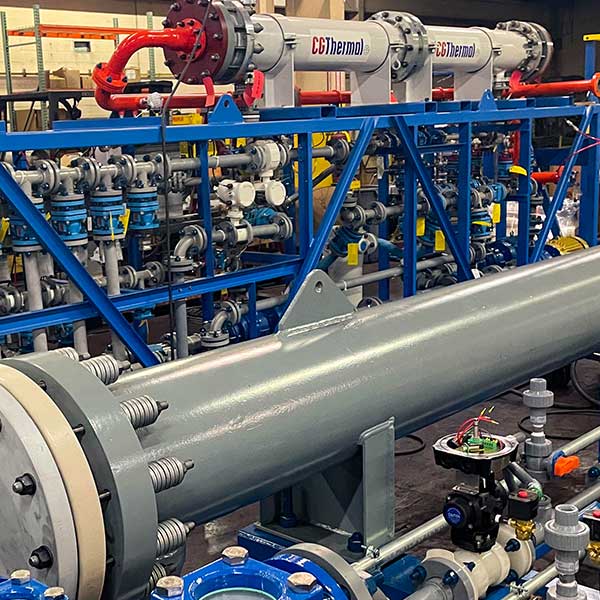
Although our Impervite® graphite excels in harsh and corrosive process streams up to certain concentrations and temperature ratings, our Umax SiC Advanced Ceramic heat exchangers are universally corrosion and erosion resistant, making them the optimal choice for sulfuric acid dilution systems. The Umax Advanced Ceramic tube will not corrode at any concentration and boasts a lifetime guarantee. Since it is 50% harder than tungsten carbide, the Umax Advanced Ceramic tube can be used at higher velocities without concern of erosion. The ability to operate at higher velocities coupled with its high thermal conductivity, makes it the most thermally efficient choice. Ultimately, the innovative tubesheet design offers superior serviceability, allowing for easy access to all tubes for cleaning and in-house repair.

Product Gallery

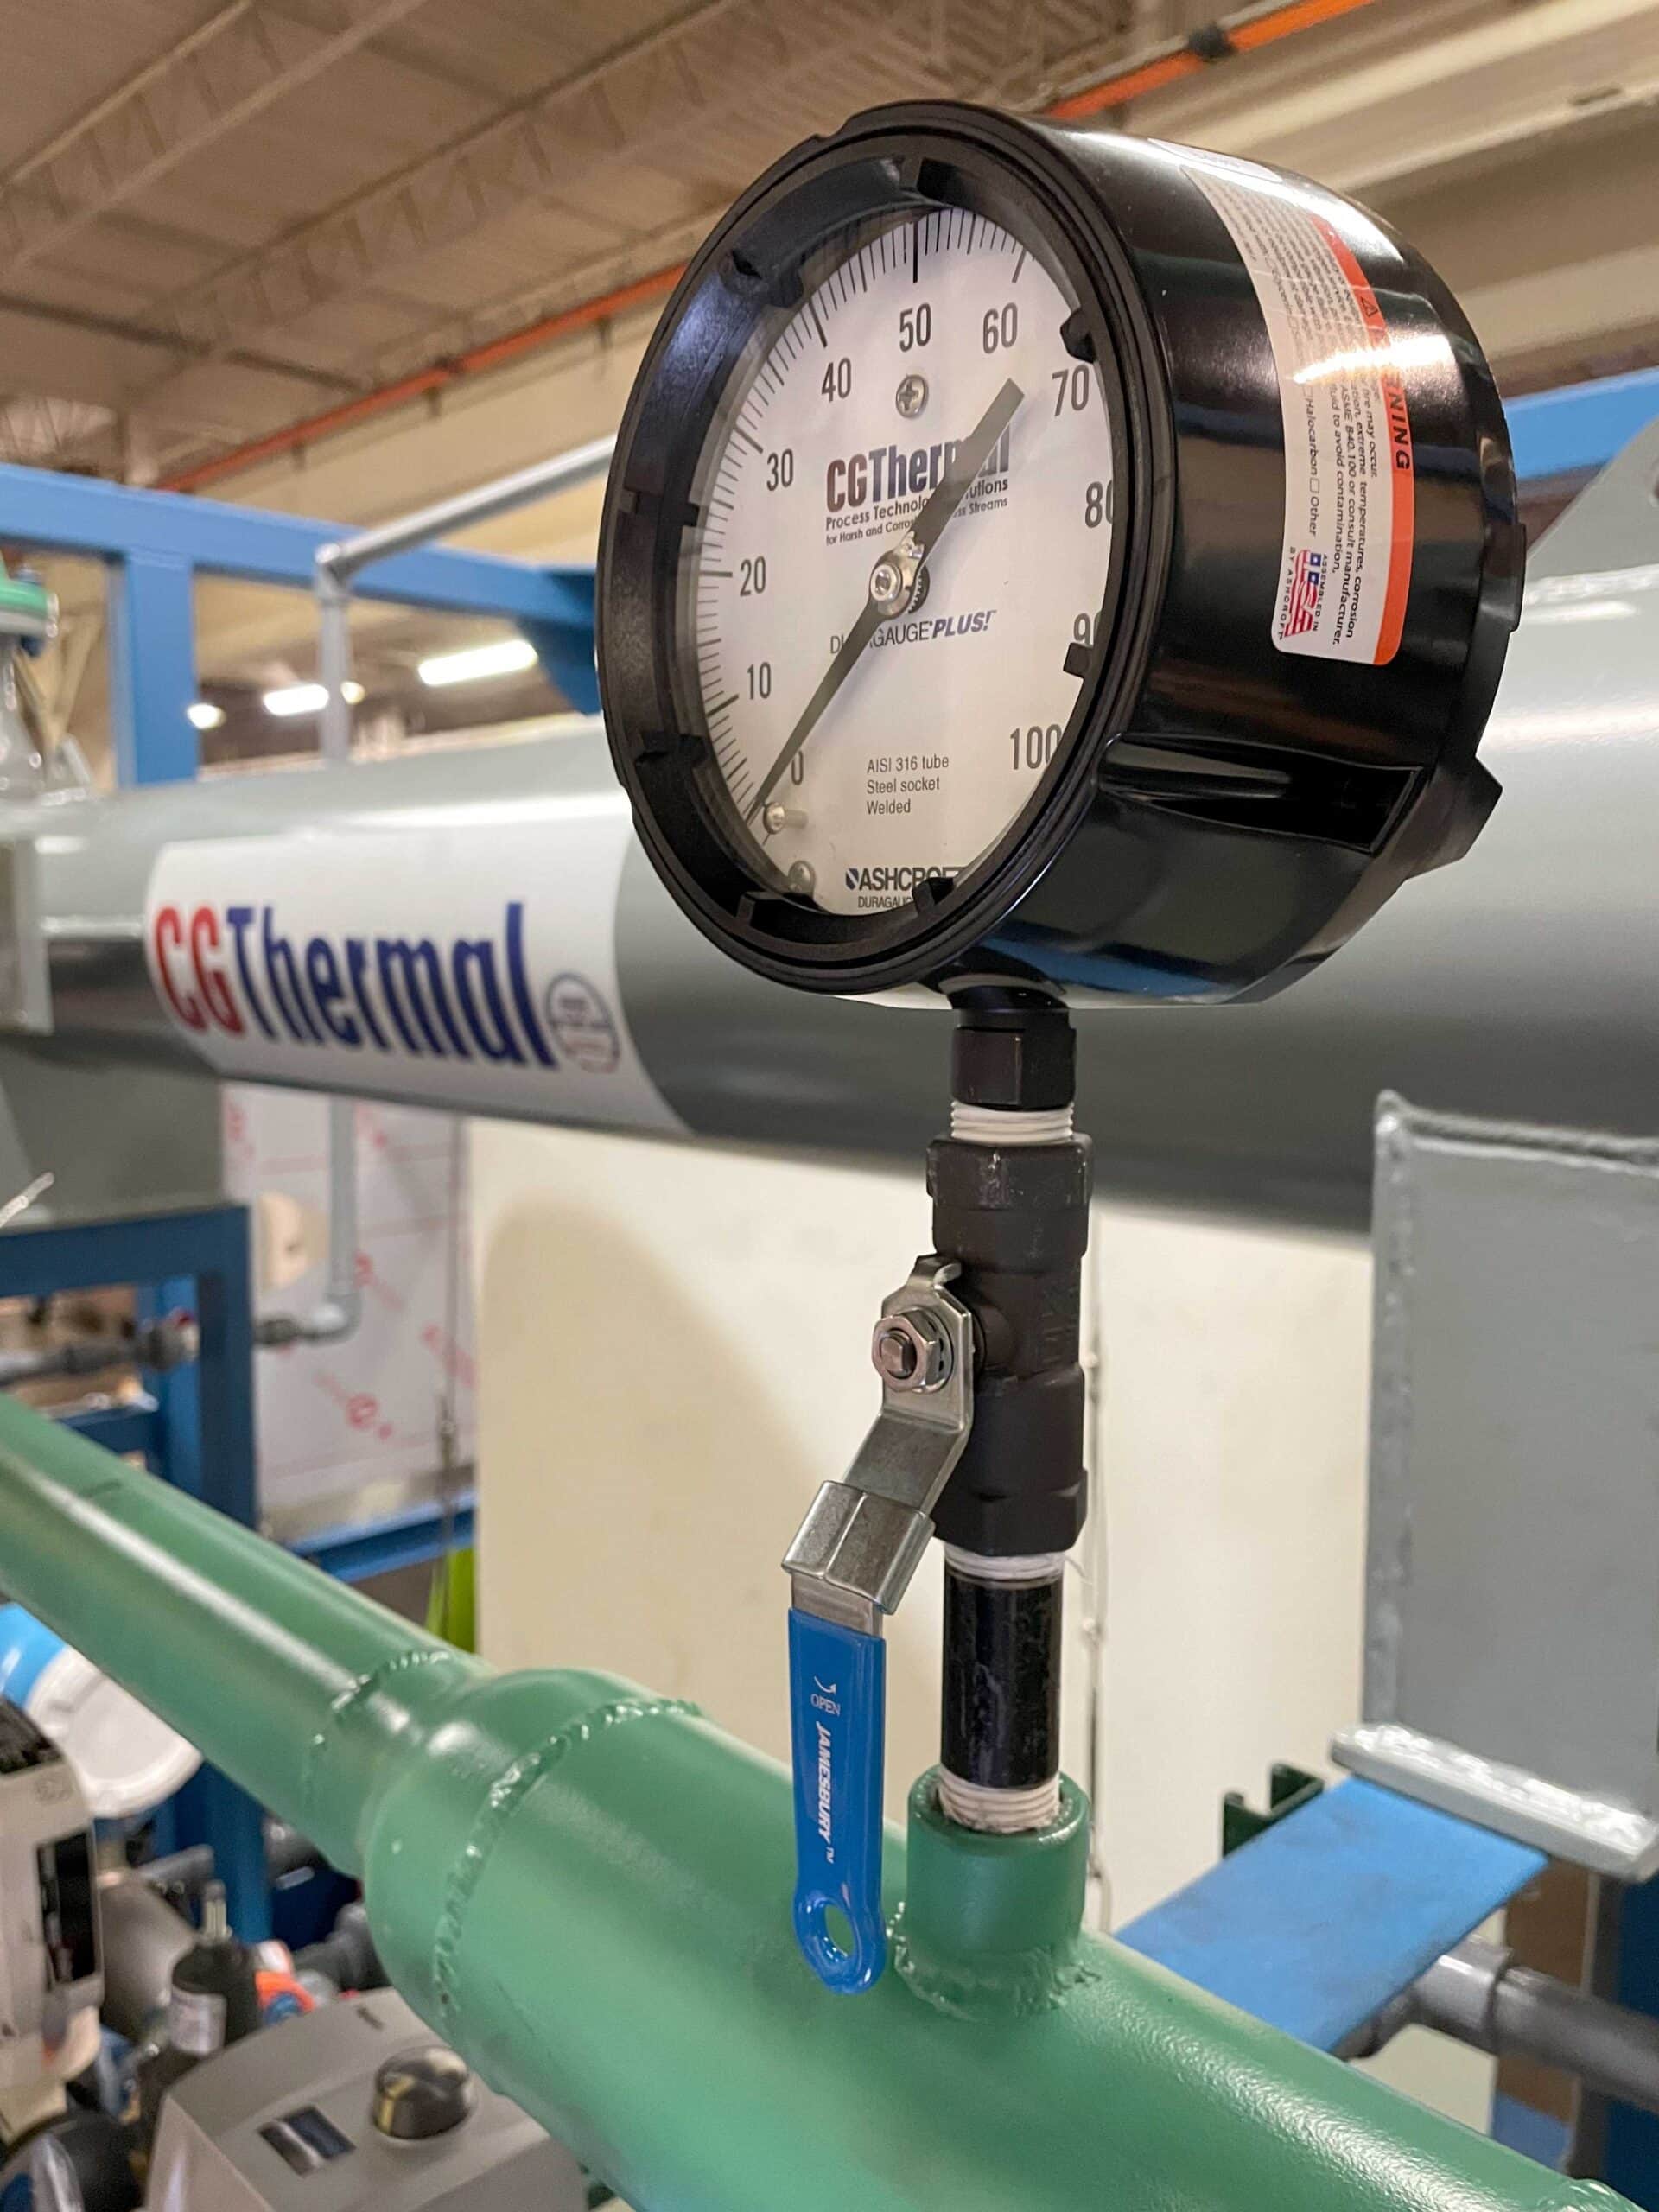

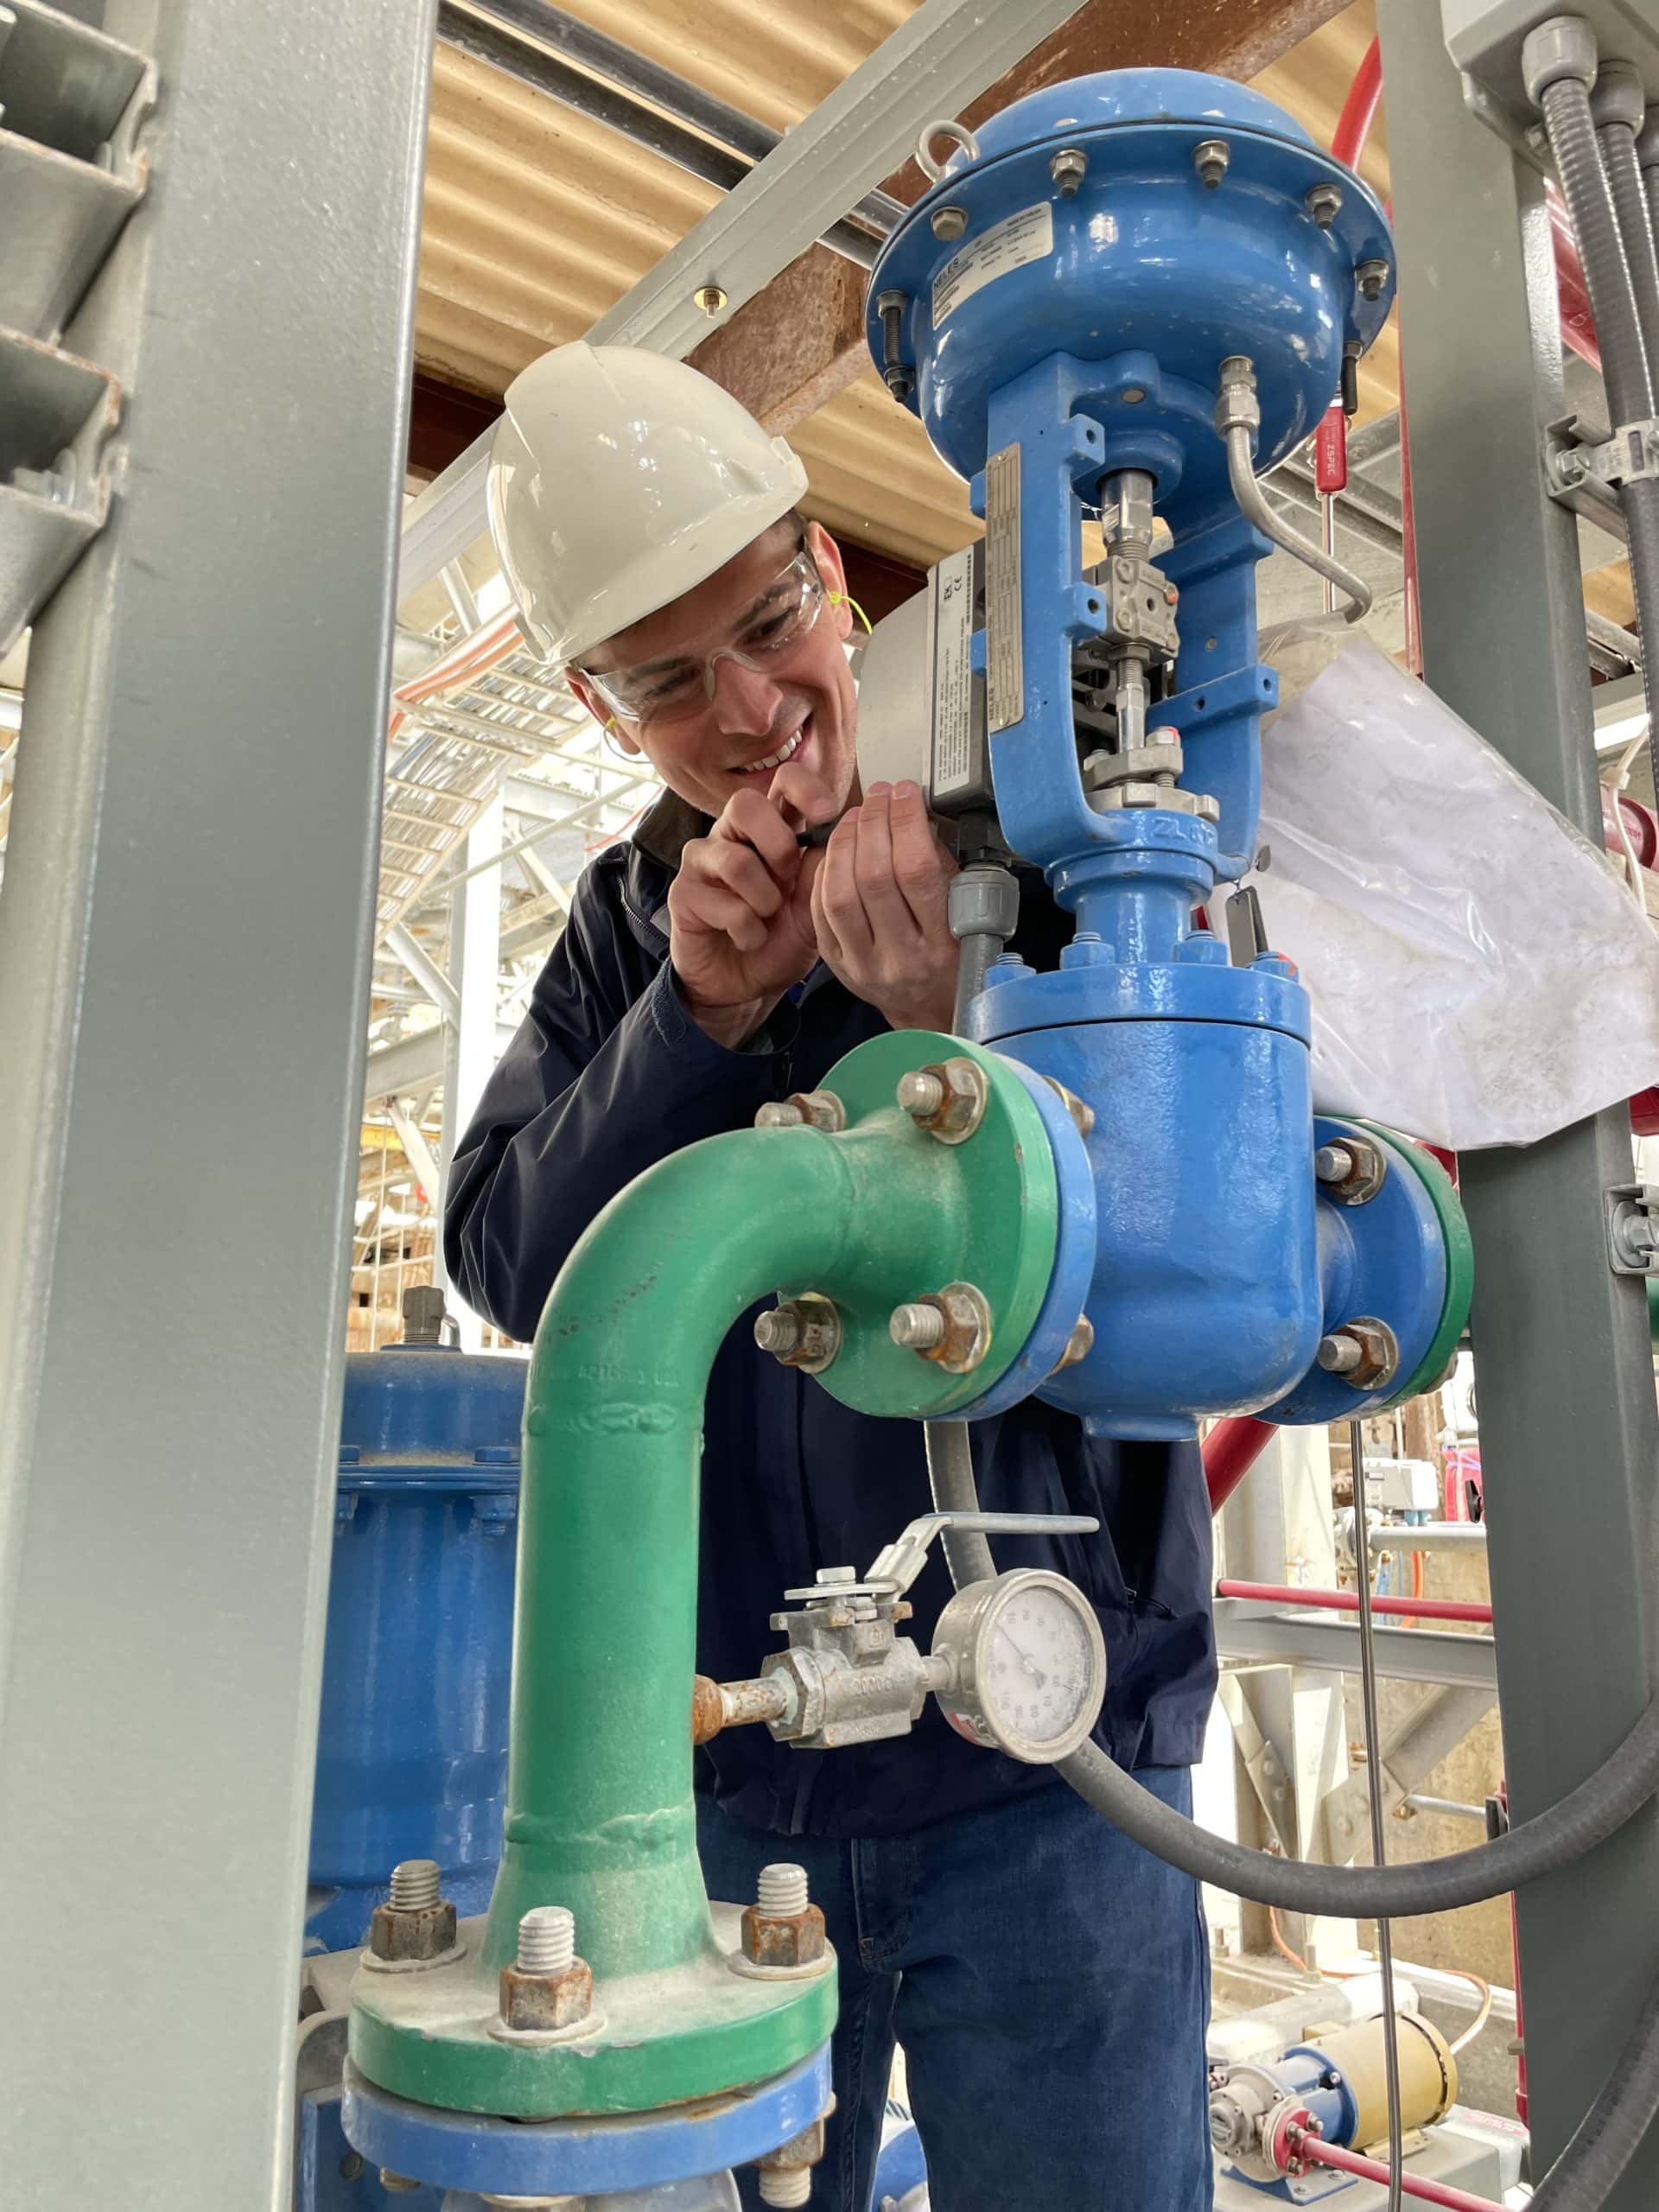
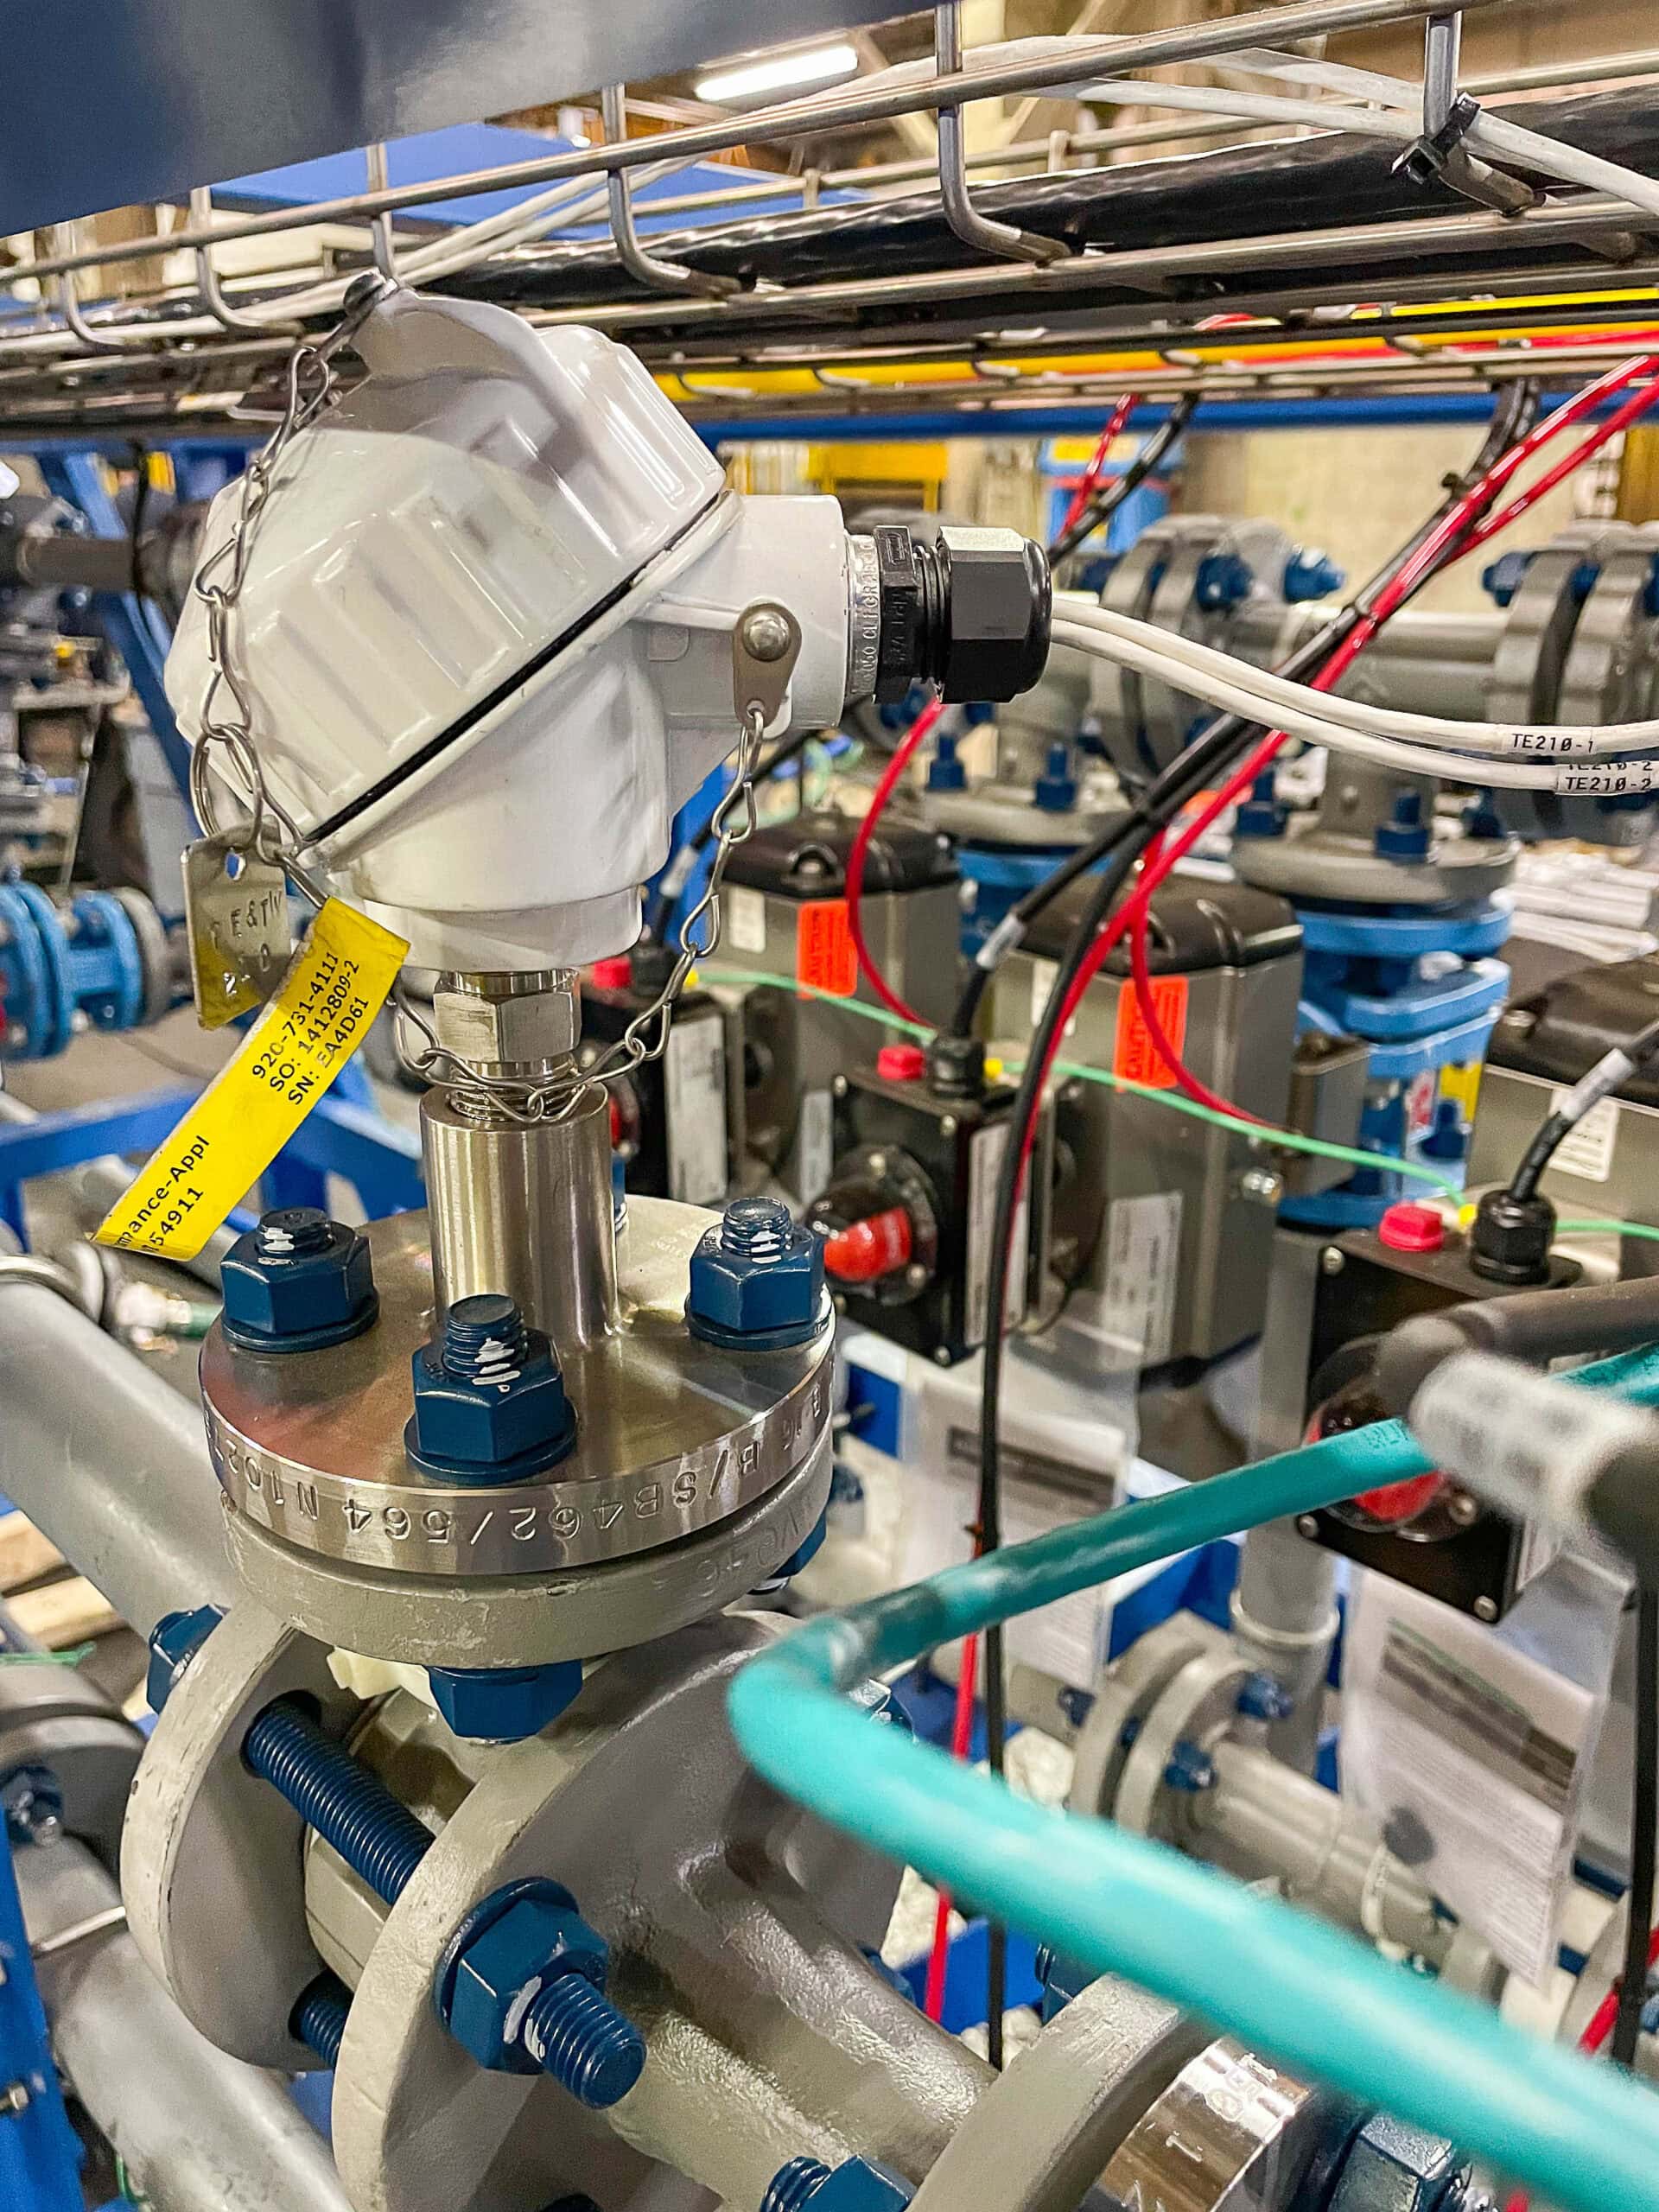
Sulfuric Acid Concentration
Recovering dilute sulfuric acid starts with understanding the process. Feed composition, contaminants, and the required acid strength guide the selection of pretreatment, evaporation equipment, and materials of construction. A well-designed system considers these factors together to prepare recovered acid for its intended reuse.
CG Thermal brings expertise in process design and corrosion-resistant equipment. Our approach considers multi-effect vacuum evaporation, heat recovery, and materials such as Impervite® graphite, Umax Advanced Ceramic, and ETFE linings to address the demands of sulfuric acid service. Download the technical bulletin, Recovering and Concentrating Dilute Sulfuric Acid, on the right for a closer look at pretreatment, system configurations, and material selection.
Extracid – Concentration / Dewatering System
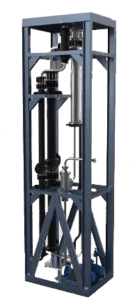 The patented Extracid system uses an innovative approach to dewater sulphuric acid from low concentrations (10%) to 97% at positive pressure. Vaporized water from the acid can be used as process steam and, as such, the Extracid process regains up to 70% of the system’s energy input. The system has a small footprint and reduces investment and operating costs.
This patented design, developed in conjunction with industry partner Wilk-Graphite, was awarded the ACHEMA 2018 Innovation of the Year. The advancements it provides include:
- Elimination of vacuum system
- Safety and Reliability with a lifetime guarantee against corrosion
- Significant energy savings with heat recovery
- High-purity product
Most sulfuric acid dewatering systems operate under vacuum due to insufficient material options. Extracid’s specialized SiC (silicon carbide) ceramic components, capable of operating at 500C+ and inert to all concentrations of sulfuric acid, provide the design freedom to safely and reliably operate at positive pressure.
Chiefly, the heart of the system is the Umax SiC block heat exchanger. The columns, compensators, and piping system are also unique designs constructed of SiC. The SiC materials of construction are proven universally corrosion resistant throughout the range of concentrations the system will see. This includes any HF that might be part of the water acid stream. Click here to learn more about our partnership.
Benefits at a glance
- Constant product concentration even at the variable inlet
- Produces process steam as a usable product
- Up to 70% energy recovery
- Low investment and operation cost
- No corrosion
- Skip mounted
- Smaller equipment envelope (footprint)
- Resistant at HF and other components
- No abrasion
- Low fouling
- Decomposes organics
- High-purity product
Sulfuric Acid Regeneration
Regeneration of the spent Sulfuric Acid is equally important in many cases for economic and environmental reasons.
 Commonly supplied at 93% concentration but diluted as a reactant or for its end purpose, its corrosivity and material compatibility will vary greatly with concentration and temperature. Although Impervite® graphite is a suitable choice in many instances, the Umax Advanced Ceramic heat exchanger is becoming the design of choice.
There are two choices for handling the spent acid – either neutralize the spent acid and dispose of it or, regenerate it to remove the impurities so the acid can be reused. With the current high demand, sulfuric acid regeneration is quickly becoming the preferred method for both economic and environmental reasons.
Material and Design Considerations:
For heat transfer applications involving sulfuric acid, materials of construction vary depending on the temperature, concentration, impurities, required service life and cost effectiveness. Common cost-effective materials include SiC ceramic, graphite, and polyphenylene sulfide (Impervite® Advanced Graphite).
Because of its resistance to corrosion in H2SO4 at all concentrations and most temperatures incurred in regeneration processes, PTFE lined steel is a commonly used for the construction of towers, separation drums, and other vessels utilized in regeneration, especially in positive pressure systems. PTFE can be rotolined for use under vacuum.
Also, several of sulfuric acid’s thermal properties require particular attention when considering heat and mass transfer systems involved in regeneration.
The viscosity of sulfuric acid varies significantly with temperature and concentration. With increased concentration and a decrease in temperature, viscosity will rapidly increase.
Additionally, vacuum conditions are frequently required when reconcentrating sulfuric acid because it has a low vapor pressure. At lower concentrations, the vapor pressure is mostly governed by the water. However, at higher concentrations, the degree of vacuum will have a more significant effect on the process temperature, which will in turn affect the energy input for the separation. This could result in higher process temperatures, reduced efficiency, and limited material options.
Electrical conductivity varies with concentration as a parabolic function, resulting in two concentrations described by the same value. Further, this condition needs to be considered in choosing measurement and control devices. Several approaches can be taken depending on the precision required.
Learn more:
Download white paper: Important Considerations in the Regeneration of Sulfuric Acid
Watch CG Thermal’s presentation from CRU-Sulphur + Sulphuric Acid 2021
Please provide us with your requirements. We look forward to using our expertise to assist you.
Sulfuric Acid Systems FAQ
What sulfuric acid process systems does CG Thermal provide?
CG Thermal designs sulfuric acid systems for a variety of applications, including but not limited to dilution, concentration, and regeneration. Our capabilities include integrated process systems, corrosion-resistant heat transfer equipment, and engineering support tailored to your application.
What factors influence sulfuric acid system design?
Acid concentration, temperature, impurities, production rate, and required product quality all influence system design. These conditions guide equipment selection, materials of construction, heat transfer requirements, and process controls.
What is the difference between sulfuric acid dilution, concentration, and regeneration?
Dilution lowers acid concentration by adding water. Concentration removes water to increase acid strength. Regeneration treats spent acid to remove or convert contaminants so the acid can be reused. The appropriate approach depends on the feed composition and intended use.
Can CG Thermal help recover sulfuric acid for reuse?
Yes. CG Thermal evaluates recovery options based on the spent-acid composition and the quality required for reuse. Depending on the application, the process may involve pretreatment, reconcentration, or regeneration.
What is a sulfuric acid dilution system?
A sulfuric acid dilution system combines concentrated acid and water to produce the concentration required by a process. An engineered system coordinates acid and water metering, mixing, heat removal, and controls to meet the specified production rate and outlet conditions.
Why does sulfuric acid dilution require cooling?
Combining concentrated sulfuric acid and water releases substantial heat. A heat exchanger removes this heat to help maintain the required outlet temperature. Cooling capacity, mixing, and feed control must be considered together during system design.
What are the benefits of diluting sulfuric acid onsite?
Onsite dilution allows a facility to purchase concentrated acid and produce the strength its process requires. This may reduce purchasing and transportation costs while providing greater control over acid concentration and availability. The potential benefits depend on consumption, delivered-acid pricing, utilities, and existing infrastructure.
Does CG Thermal offer pre-engineered sulfuric acid dilution packages?
Yes. DiluteMax Pro™ sulfuric acid dilution packages combine controlled metering, mixing, heat removal, instrumentation, and automated controls in an integrated skid-mounted system. They provide a defined starting point for facilities with recurring dilution needs.
When should I consider a custom sulfuric acid dilution system?
A custom system may be appropriate when capacity, concentration, temperature, layout, or control requirements fall outside a pre-engineered package’s operating range. CG Thermal can also provide engineering support or individual components to complement your in-house capabilities.
What materials are used in sulfuric acid systems?
Materials are selected for the specific acid concentration, temperature, impurities, and service conditions. Depending on the application, CG Thermal’s systems may incorporate Umax Advanced Ceramic silicon carbide, Impervite® graphite, and fluoropolymer-lined equipment.
What information does CG Thermal need to evaluate my application?
Start with the process objective, feed composition, required product concentration, and production rate. Operating temperatures, available utilities, site constraints, and existing equipment help define the system. If some details are still being developed, our team can help establish the remaining requirements.
Can a dilution system integrate with existing plant equipment?
Yes. CG Thermal can design a dilution system to connect with existing acid storage, water supply, finished-product tanks, transfer equipment, and plant controls. Our team reviews the available infrastructure and connection requirements to define the scope of supply and any additional equipment needed.